



Join our Agent Partners for Premium Coatings and Business Growth.
KAIDA PAINT®
Industrial Coatings Manufacturer & Global Flooring Solutions Contractor
Showing all 8 results
-

E550 Solvent-based Epoxy Topcoat
Read more -
E552 Anti Static Self-leveling Epoxy Coating
Read more -
E556 Water-based Epoxy Finish
Read more -
E8300 Self-leveling Epoxy Floor Top Coat
Read more -
E8302 Solvent-Free Self-Leveling Epoxy Floor Top Coat
Read more -
E8308 Epoxy Colored Sand Self-Leveling Topcoat
Read more -
E850 Epoxy Orange Peel Floor Finish
Read more -
E860 Spreadable Epoxy Top Coat
Read more
Raw Material Selection
Formulation and Blending
Batch Testing and Quality Control
Manufacturing and Packaging
Color Matching and Sample Approval
VOC Compliance and Low-VOC Systems
Technical Support and On-Site Installation
Export Packing and Global Delivery
Raw Material Selection
Epoxy resins, curing agents, pigments, fillers and solvents are sourced from established international chemical suppliers. Every incoming batch is inspected and released to production only after it passes the factory’s incoming-material check. Each batch record is filed so that a finished product can be traced back to the materials it was made from.
Formulation and Blending
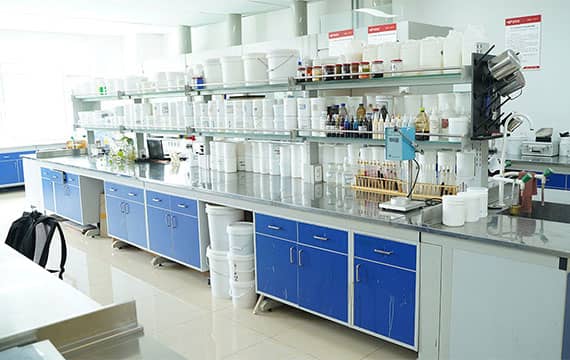
Formulations are developed and adjusted in the factory laboratory. Each production run is blended to a recorded formula with a fixed mixing ratio and mixing sequence, and the batch is checked for viscosity and gel time before it is released for filling. Formulations are tuned to specific performance targets – adhesion, chemical resistance, abrasion resistance or VOC content – rather than to a single generic specification.
Batch Testing and Quality Control
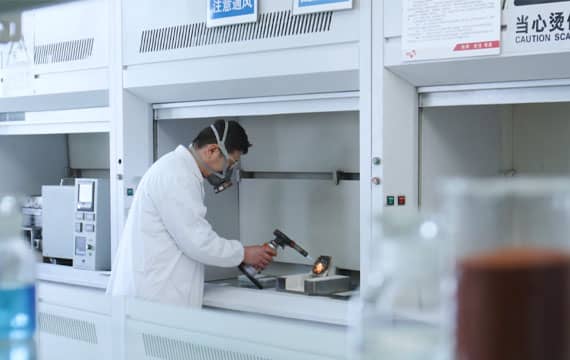
Each batch is tested before packing. Testing covers the properties that determine how the coating performs on site – adhesion, abrasion resistance, hardness, gloss level and solids content – against the product’s technical data sheet. Test reports are issued per batch and can be supplied with the shipment.
Manufacturing and Packaging
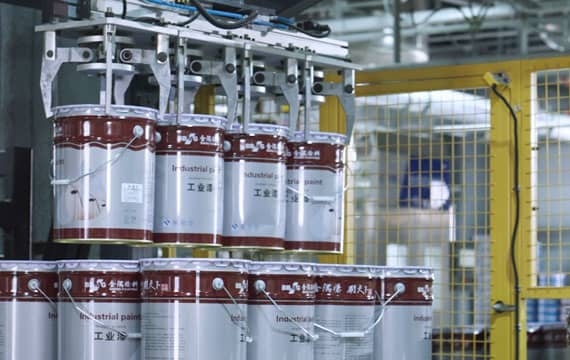
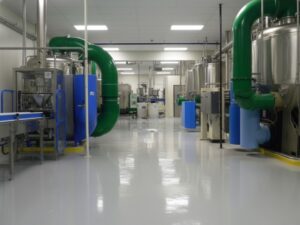
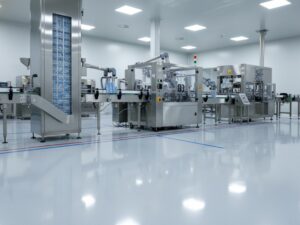
Production runs on the factory’s coating lines, where the coatings are mixed in large batches and filled into pails or drums. Every container is labeled with the product code, batch number and production date, and the label carries the KAIDA PAINT® brand, so a delivered container can always be matched back to its batch record.
Color Matching and Sample Approval
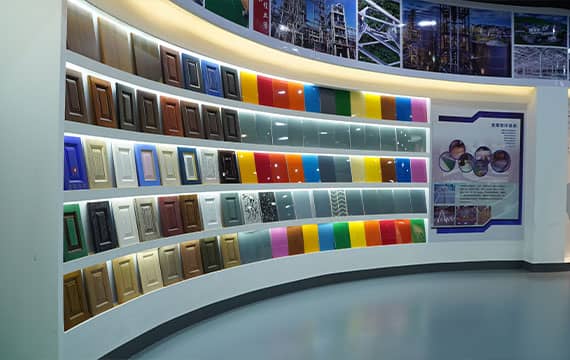
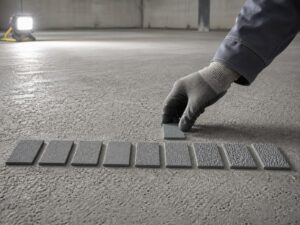
Color matching is carried out in-house against the factory’s standard color range. Where a project needs a specific shade, a color chip is prepared and submitted to the customer for written approval before production starts, so the delivered material matches what was approved.
VOC Compliance and Low-VOC Systems
Water-based and solvent-free systems are formulated to meet the VOC limits that apply in the destination market. The VOC content of each product is stated in g/L on its technical data sheet, so a specifier can check compliance against the regulation for their own project rather than relying on a general claim.
Technical Support and On-Site Installation
Technical support covers system selection, substrate assessment, application guidance and fault diagnosis – before, during and after delivery. Where a project requires it, application is carried out by installers, and the team that advised on the specification stays involved during application.
Export Packing and Global Delivery
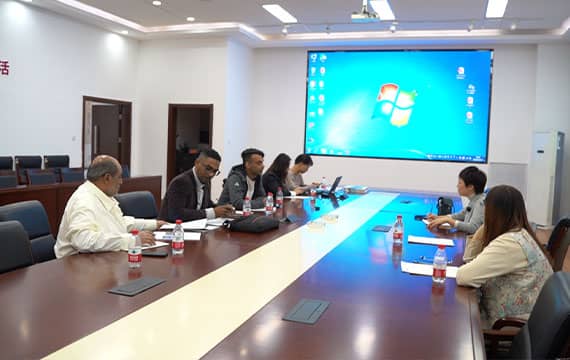
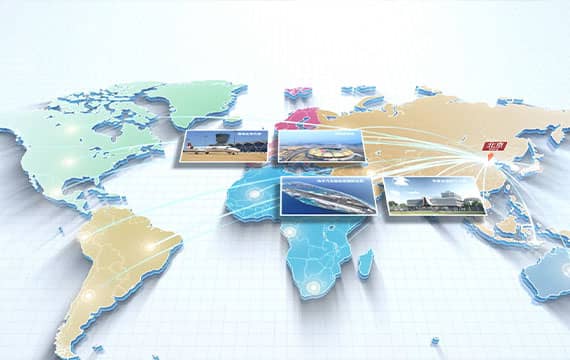
Orders are packed for export with the documents a project needs – technical data sheet, safety data sheet and batch test report. Packing and labeling are adjusted to the requirements of the destination market. Recent projects shipped from the factory include a 10,000 m² food plant floor in Venezuela, an industrial flooring project in Sweden, and a battery plant renovation in Hungary.
KAIDA supplies epoxy floor coatings and industrial coatings for industrial and commercial projects. KAIDA PAINT® is the export brand of Tianjin Kaida Tech Co., Ltd.; coatings are manufactured by JINYU in China.
© 2023 KAIDA PAINT. All Rights Reserved -
Design by KAIDA
We've detected you might be speaking a different language. Do you want to change to:
 English English
 Spanish
 Portuguese
 Arabic
 French
 Italian
 Russian
 Indonesian
 Swedish